If you’ve ever had to troubleshoot fluid or gas control systems—whether in a manufacturing line, a commercial HVAC unit, or even a grocery store’s refrigeration setup—you’ve probably bumped into a solenoid valve. These unassuming components are the workhorses of industrial and commercial process control, but most people don’t stop to ask why they work so reliably, or what makes a small part inside them so critical. As a solenoid valve supplier who’s spent thousands of hours working with end-users, maintenance techs, and design engineers, one question comes up more than almost any other: What role does the diaphragm play in a solenoid valve? It’s not a flashy part, but skip the diaphragm, and your valve’s not going to open or close when you need it to. Let me break this down like I would for a new technician walking through our warehouse, no overly complex jargon, just real-world context that makes sense. Solenoid Valve
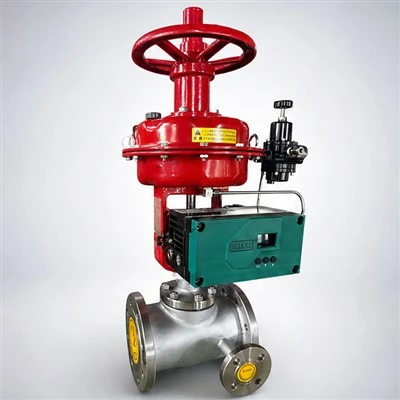
First, let’s start with a quick reminder of what a basic solenoid valve does, because if you’re here, you probably already know, but it sets the stage. A solenoid valve is an electromechanical switch for fluid (water, oil, coolant) or gas (air, natural gas, nitrogen) flow. When you send an electrical signal to the solenoid coil—usually a low-voltage DC or high-voltage AC pulse—a magnetic field is created. That magnetic field pulls a small, movable core (called a plunger or armature) inside the valve body, and that’s what shifts the valve from its normally closed (NC) or normally open (NO) state. That part is straightforward, but here’s where the diaphragm comes in: it’s the barrier between the electrical side (the coil and armature, which are exposed only to air, not process fluid) and the actual flow path where your water or gas is moving. Without that barrier, process fluid would leak into the coil, short out the electronics, and turn your simple valve replacement into a full electrical system repair. That’s the most basic, non-negotiable role: seal integrity.
But the diaphragm does a lot more than just keep dirty water out of the solenoid. Most solenoid valves used in industrial and commercial applications aren’t direct-acting—they’re pilot-operated. If you’ve ever used a hose bib that needs a little extra pressure to open, that’s the same principle at play. Pilot-operated valves use the pressure of the process fluid itself to open and close the main flow orifice, which means they can handle much higher flow rates and higher pressure differentials than small direct-acting valves. And the diaphragm is the master of that pressure balance. Let’s walk through how that works step by step for a normally closed pilot-operated solenoid valve, since that’s the most common type you’ll find.
When the valve is in its resting, de-energized state (no electrical signal), two things happen to keep it closed. First, the diaphragm sits on top of a small main flow orifice, and it has two small pilot holes drilled through it—tiny, just big enough to let process fluid seep through. On top of the diaphragm, there’s a small chamber called the pressure equalization chamber, and when the valve is closed, fluid flows through those pilot holes into that chamber, building up pressure that’s almost equal to the pressure of the main line feeding the valve. Since the area of the diaphragm exposed to that equalized pressure is larger than the area of the main orifice, the force pushing down on the diaphragm from the equalized chamber is stronger than the force pushing up on the diaphragm from fluid trying to flow through the main orifice. That means the diaphragm stays pressed tight against the main orifice, holding the valve closed, even if the line pressure is 100 PSI or higher.
Now, when you send the electrical signal to the solenoid coil, the armature pulls up a small pilot plunger that’s sitting right next to that pressure equalization chamber. That plunger opens a tiny pilot vent hole, releasing the pressure trapped inside the equalization chamber. Within milliseconds, the pressure in that chamber drops below the pressure in the main line below the diaphragm. The balance of forces flips: now the force pushing up from the main line on the diaphragm is stronger than the force pushing down from the low-pressure equalization chamber. The diaphragm lifts off the main orifice, and fluid or gas flows freely through the valve. That’s the pilot-operated magic, and the diaphragm is the part that makes all that pressure balance possible. If the diaphragm was rigid, or if it leaked, or if it was the wrong thickness, that pressure wouldn’t equalize correctly, and the valve would either fail to open, fail to close, or leak around the edges.
Let me tell you a true story to illustrate how important this is, because numbers on a spec sheet don’t always stick. A few years back, we had a customer in the food and beverage industry that makes bottled water, and they were having constant issues with their production line’s fill valves. They were getting 20 to 30 unplanned stops a week, which was costing them thousands of dollars in lost production per hour. They’d replaced solenoid coils, armatures, even the entire valve bodies, but nothing worked. They brought the broken valves to our shop, and the first thing our lead tech noticed was that the diaphragms were wearing out in less than three months. Turns out, they were using standard nitrile diaphragms for their fill water, which was chlorinated at a high level for food safety. Nitrile is fine for mild chlorinated water, but constant exposure to high levels of chlorine eats away at the rubber, making the diaphragm porous. Once it was porous, fluid would seep through the pilot holes unevenly, so the pressure equalization never worked right. The valve would either take too long to open, or it would leak when closed, causing overfilling on the line. We swapped their standard nitrile diaphragms for EPDM ones, which are rated for much higher chlorine resistance, and we also adjusted the pilot hole size to match their line pressure. Since that change, their unplanned stops dropped to less than one a month. That’s how much of a difference the right diaphragm makes—not just for function, but for reliability and uptime.
The diaphragm isn’t one-size-fits-all, either, which is why as a solenoid valve supplier, we spend so much time asking customers about their specific application details when they call to order a replacement part. Diaphragms are made from different materials, each suited for different process fluids, temperatures, and pressure ranges. Let’s break down the most common materials and what they’re used for, so you can understand why picking the right one matters:
- Nitrile (Buna-N): The most common general-purpose diaphragm, good for mild water, oil, and petroleum-based fluids. It works well in temperatures from -40°F to 250°F, but as I mentioned, it’s not great for strong acids, bases, or high-chlorine water.
- EPDM: Great for water, steam, and many acids, bases, and ozone. It’s more resistant to harsh chemicals and higher temperatures, up to 300°F, which makes it a top choice for HVAC, food and beverage, and pharmaceutical applications.
- Viton: For extreme chemical resistance, this is the go-to. It works with strong acids, fuels, and gases, and can handle temperatures up to 400°F. It’s pricier, but if you’re working with corrosive fluids like industrial solvents or natural gas with high sulfur content, it’s non-negotiable.
- PTFE (Teflon): Used for ultra-pure applications, like semiconductor manufacturing or pharmaceutical processes where contamination is a risk. It’s chemically inert, so it won’t react with almost any fluid, but it’s stiffer than rubber diaphragms, so it’s mostly used in low-pressure applications.
We also use different diaphragm designs for different valve types. Some are flat diaphragms, which are simple, low-cost, and work well for low pressure. Others are convoluted diaphragms, which have ridges or folds that let them move more smoothly, with less friction, which is important for high-cycle applications (like valves that open and close hundreds of times an hour). Convoluted diaphragms also have a longer lifespan in applications with rapid pressure changes, because they don’t flex as much as flat diaphragms, which reduces wear over time.
Another key role of the diaphragm, that I don’t see many people talk about, is noise reduction. If you’ve ever stood next to a solenoid valve as it cycles, you know that loud, sharp click and rattle that happens when the armature snaps closed. A diaphragm acts as a cushion between the moving armature and the valve body, absorbing that impact. That might seem like a small thing, but in commercial settings like hospitals, schools, or office buildings, where noise is a concern, it’s a huge benefit. Diaphragms also help reduce water hammer—those sudden, damaging pressure spikes that happen when a valve closes quickly. The flexible diaphragm can give a tiny bit when the pressure changes, softening that spike and reducing wear on the entire valve and the piping system around it. I’ve had customers tell us they switched to diaphragm-type solenoid valves to meet OSHA noise standards, and they saved thousands in piping repairs from water hammer.
Now, let’s address a common misconception: do all solenoid valves use diaphragms? The short answer is no. Direct-acting solenoid valves, which are small, low-flow, and operate at very low pressure (usually less than 10 PSI), don’t need a diaphragm to use pressure balance, because the armature is strong enough to pull the plunger directly against the fluid pressure to open the valve. These valves usually have a simple seal or O-ring instead of a diaphragm. But for anything over 10 PSI, or for valves that handle flow rates higher than a few gallons per minute, a diaphragm is non-negotiable. Direct-acting valves have their place—like in small ice makers or fountain dispensers—but if you’re working with industrial processes, large HVAC systems, or any application where you need reliable, consistent flow control at higher pressure, diaphragm solenoid valves are the only way to go.
As a solenoid valve supplier, I see too many customers cut corners on diaphragms, usually because they go for the cheapest part instead of the right part for their application. Last year, a small manufacturing shop called us in a panic because their boiler feed valves were failing every two weeks. They’d been buying generic valves from a big box industrial supply store for half the price of our products, and they thought they were saving money. The problem? The generic valves used a low-grade neoprene diaphragm that couldn’t handle the 275°F steam and high mineral content of their feed water. Every two weeks, the diaphragm would degrade, leak, and let steam escape, triggering alarms and shutting down their boiler. When they switched to our standard diaphragm valve with an EPDM diaphragm rated for steam and high-temperature water, they haven’t had a failure in over a year. That’s the ROI of choosing the right diaphragm—it’s not just about upfront cost, it’s about avoiding unplanned downtime, repair bills, and lost revenue.
So, to circle back to the original question: what is the role of the diaphragm in a solenoid valve? It’s not just a seal. It’s the barrier that keeps your electronics safe from process fluid. It’s the part that enables the pressure balance that lets pilot-operated valves work at high flow and high pressure. It’s the component that determines how well your valve cycles, how long it lasts, and how reliable it is in your specific application. It’s also a key factor in reducing noise and protecting your piping from damage from water hammer. Every other part of the solenoid valve—coil, armature, valve body—depends on the diaphragm working as designed. Without it, you don’t have a solenoid valve; you have a metal and plastic part that can’t control flow for more than a few cycles.
If you’re working on a project, troubleshooting a failing valve, or just trying to figure out the right solenoid valve for your needs, the diaphragm is the first thing to get right. Too many people focus on the valve’s voltage or flow rate, but the diaphragm material and design is what will make or break performance in the long run. As a solenoid valve supplier that’s been in this business for over 15 years, we don’t just sell valves—we help our customers pick the right parts for their specific jobs, and that starts with asking the right questions about their process fluid, pressure, temperature, and cycle rate. If you’re dealing with a valve that’s leaking, failing to open or close, or just not working as reliably as it should, chances are the diaphragm is the culprit. We’ve seen it a hundred times.
If you need help picking the right valve for your application, or if you need replacement parts and expert advice, don’t hesitate to reach out. Our team has years of experience working with all types of industries, from food and beverage to pharmaceutical to industrial manufacturing, and we can help you find the solution that keeps your systems running smoothly without unnecessary downtime or repair costs.
Globe Valve References
- “Solenoid Valve Design and Application Guide.” Fluid Controls Institute, 2021.
- “Diaphragm Material Selection for Process Control Valves.” International Society of Automation (ISA), 2020.
- “Pilot-Operated Solenoid Valves: Pressure Balance and Performance.” Valve Magazine, Vol. 47, No. 2, 2019.
- “Fluid Seal Technology for Industrial Control Components.” American Society of Mechanical Engineers (ASME), 2018.
Shandong Yuhong Valve Co., Ltd.
Shandong Yuhong Valve Co., Ltd. is one of the most professional solenoid valve manufacturers and suppliers in China. With abundant experience, we warmly welcome you to wholesale high quality solenoid valve at competitive price from our factory. Good service and punctual delivery are available.
Address: Intersection of Chuangye Avenue and Huanghe Road, Zhangdian District, Zibo City, Shandong Province
E-mail: info@yuhong-valve.com
WebSite: https://www.yh-controlvalve.com/
