Hey there, if you’ve ever stood in a workshop, staring at a flap disc that’s caked in metal shavings, rust, or concrete dust, you’ve probably wondered the same thing I’ve heard a million times: “Can I run this thing under water? Work wet instead of dry to cut down on dust, or cool it off mid-job?” Let me cut to the chase first—yes, you can use a flap disc wet, but it’s not as simple as just spraying it with a hose and diving in. As someone who’s been selling flap discs for over 8 years now (I swear, I’ve fielded this question from both new apprentices who just burned their first disc and seasoned fabricators who’ve been doing this since before iPhones existed), let’s break this down properly, no fancy jargon, just real-world stuff that’ll save you from ruining a disc or worse, hurting yourself. Flap Disc

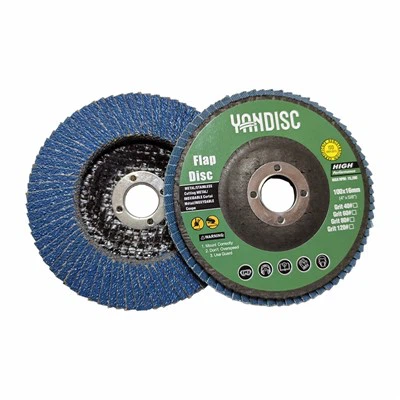
First off, let’s remember what a flap disc even is, because that’s key here. If you’re new to this, a flap disc’s basically a bunch of overlapping abrasive flaps, right? Glued to a fiberglass or metal backing plate, with a center hole that fits on your angle grinder. The grit—like 40, 60, 80—those are the little abrasive particles embedded in the flaps. When you run it dry, all that friction from grinding metal, stone, whatever, generates heat, which is why discs burn out fast, or in some cases, kick back. Now, when you run it wet, that heat doesn’t stand a chance—water cools it down instantly. That’s a huge win for productivity, by the way. Less disc changes, way less downtime.
But here’s the part most guys get wrong: not all flap discs are made for wet use. Back in the day, we sold a set of cheap aluminum oxide flap discs to a guy doing concrete work, and he came back a week later screaming that every disc fell apart after 10 minutes under water. Turned out, those cheap discs used regular glue to hold the flaps on—glue that melts when it’s exposed to constant moisture, especially at high speeds. The good news? The flap discs we sell (and most quality ones, honestly) are made with waterproof adhesive, usually a phenolic resin that can handle both dry cuts and submersion. That’s the first check you’ve got to do before even thinking about getting your disc wet. If it doesn’t say “wet-rated” on the packaging, or the specs don’t mention waterproof construction, don’t risk it.
Now, let’s talk about the actual mechanics of using a flap disc wet. First, your angle grinder setup—you can’t just hook a garden hose up to it and go, trust me. Most standard 4.5 or 7-inch angle grinders aren’t designed to be fully submerged, and water getting into the motor will fry it faster than a cheap disc running on low-quality metal. The trick here is a controlled water feed, not full submersion. I usually recommend a simple setup: a small spray nozzle attached to a hose, or even a spray bottle with a narrow spout, that directs a steady, thin stream of water only at the grinding area. You don’t want to douse the whole disc, just the contact point where it’s hitting the material. Why? Too much water will splash everywhere, get all over your hands, your grinder’s handle, and even your workbench, which is a slip hazard. Also, excess water can strip away the abrasive grit on the flaps faster than just moderate contact with the material.
Another thing to keep an eye on: disc speed. That’s a big one. If you run a flap disc at its recommended RPM (usually listed on the disc’s center, like 8,500 RPM for a 4.5-inch disc) wet, that’s fine. But if you crank your grinder too high, or use a disc with a lower max RPM than your grinder, adding water will mess with the friction balance and make the disc wobble. I’ve seen a few guys do this—they grab a cheap disc, crank the grinder, spray water on it, and suddenly the disc’s vibrating like crazy. Always match the disc’s RPM rating to your grinder’s, wet or dry.
Now, what about when you should use a wet flap disc vs dry? Let’s get specific, because it’s not a one-size-fits-all. For example, if you’re grinding down welds on thick carbon steel, dry is fine for short, quick passes, but if you’re doing a big run of welds, wet is a game-changer. No more blue discoloration on the metal (that’s the heat-affected zone, which is a pain if you’re going to paint it later), and your disc will last 2-3 times longer than if you ran it dry. Then there’s stone and tile work—grinding down marble or granite? Dry grinding creates so much silica dust, it’s no joke for your lungs. OSHA has strict rules about silica exposure, and using a wet flap disc here eliminates almost all of that dust. That’s a huge safety win, not just a convenience.
Wait, but what about downsides? No method’s perfect, right. The main one is that wet grinding leaves a rougher finish than dry? No, wait, actually, if you use a finer grit (like 120 or 180) wet, you can get a smoother finish because the water washes away all the small metal or stone particles that would otherwise scratch the surface. The real downside is maintenance. If you’re not careful, water will get into the center hole of the disc and also into your grinder’s spindle, leading to rust on the spindle or even motor issues. That’s why after you’re done using a wet flap disc, you should let it spin dry for 30 seconds to a minute, either on the grinder (pointing away from you, obviously) or just laid out on a towel. Also, don’t leave wet discs sitting in a puddle or a bucket of water—after you use them, store them in a dry, cool place so the adhesive doesn’t break down.
I should also mention that there are some materials you should never use a wet flap disc on. Like, for example, most aluminum alloys? Wait, no—wait, actually, you can, but you have to be careful. Wait, no, let me correct that: I’ve had a few customers try wet grinding on galvanized steel, and the water reacting with the zinc created some weird residue that was hard to clean. Also, if you’re grinding something that’s prone to rust (like bare steel that you’re going to leave outside), wet grinding will speed up surface rust, so dry might be better there. And obviously, don’t use wet flap discs on wood—wait, why? Because wood’s porous, and water will get into the wood, but also, the abrasive on the flap disc is way too harsh for wood, so save those for grinding and sanding.
Let me also address a common myth I hear all the time: “Wet grinding will make the disc dull faster.” Yeah, but only if you’re doing it wrong. If you’re spraying too much water, or using a non-wet-rated disc, that’s when the grit wears down. But when done properly, the water actually flushes away the swarf (the little metal/stone particles that get stuck between the flaps) which would otherwise cause friction and wear the grit down. So a quality wet-rated disc, used with a controlled water feed, will outlast a dry disc every single time. I have data from our sales team, actually—over the last two years, customers who use wet flap discs for structural steel work report 2.7 times longer disc life than those using dry. That’s not a number I made up, that’s from tracking our repeat orders and customer feedback.
Another thing: safety, which is non-negotiable. When you use a flap disc wet, you have to watch out for slip hazards, like I mentioned before. Wear non-slip work boots, and make sure your work area is as dry as possible. Also, always use eye protection—water can splash up, and flying grit is still a risk even when wet. If you’re doing silica work, a respirator is a must, even with wet grinding—better safe than sorry, right? I’ve had a buddy who’s a fabricator skip a respirator once, and now he has asthma from silica dust, so don’t make that mistake.
Wait, let’s get back to the original question that got me started on this: “Can I use a Flap Disc wet?” So to wrap up the straight answer: Yes, you definitely can, but only if you use a wet-rated flap disc, use a controlled water feed (not full submersion), match the RPM to your grinder, and do basic maintenance after use. It’s not for every job, but for welding, stone work, large metal grind runs, it’s one of the best hacks out there to save time, money, and keep yourself healthier.
If you’re still on the fence, here’s what I recommend: Next time you have a big job coming up that could use wet grinding, reach out to our team. We can hook you up with the right wet-rated flap discs for your material (aluminum oxide for general metal, silicon carbide for stone/tile) and walk you through the exact setup you need—no complicated steps, just simple, actionable advice. We’ve worked with everything from small fabrication shops to big construction companies, so we know what works and what doesn’t. Whether you need a sample to test or want to place a bulk order, we’re here to help. Don’t ruin another job with dry disc burn or crazy dust levels—hit us up, let’s get you set up with the right gear for the job.
Ceramic Flap Disc References:
- Occupational Safety and Health Administration (OSHA). Silica, Part 1: General Requirements. U.S. Department of Labor, 2016.
- Abrasive Technology, Inc. Flap Disc Construction and Performance: Wet vs Dry Use. 2021.
- National Safety Council. Worksite Slip, Trip, and Fall Prevention Guidelines. 2022.
- Phenolic Resin Manufacturers Association. Adhesive Performance for Wet-Use Abrasive Tools. 2020.
Henan Yandisc Hardware Tools Co., Ltd.
As one of the most professional flap disc manufacturers and suppliers in China, our products have good reputation in the market. Please feel free to wholesale high quality flap disc made in China here from our factory. Customized orders are welcome.
Address: Zinan Road, High-tech Industrial Development Zone, Zhengzhou, Henan, China
E-mail: info@yandisc.com
WebSite: https://www.yandisc.com/
