If you’ve ever stood on a production floor watching a cryogenic system shut down because a valve failed, you know how costly and dangerous that mistake can be. As a ball valve supplier with 17 years of experience serving industries from liquefied natural gas (LNG) processing to pharmaceutical cold chain distribution, I’ve seen too many projects go sideways because someone picked the wrong cryogenic valve. It’s not just about grabbing a valve that “works in cold temps”—cryogenic service is a unique set of challenges, and getting the selection right boils down to matching a valve’s specific design to your application’s needs. Let me walk you through the practical, science-backed steps I share with every customer who calls looking for a cryogenic ball valve, so you avoid the same headaches we’ve fixed over and over. Ball Valve
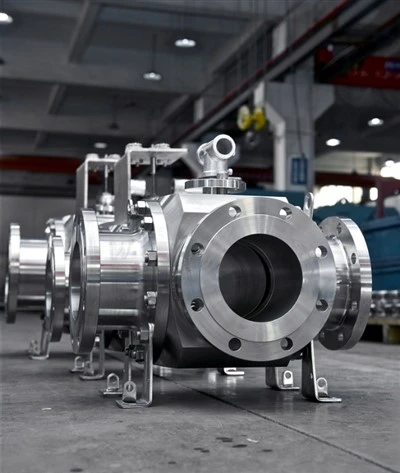
First, let’s clarify what “cryogenic” actually means for valves. Most people think it’s just “very cold,” but for our industry, cryogenic service means handling fluids at or below -150°F (-101°C). That’s not just cold enough to make water ice instantly—it’s cold enough to embrittle most standard metals, shrink seals and packing materials to the point they leak, and even change the way a valve’s components fit together. A standard general-purpose ball valve might work at room temperature or even 30°F, but drop it to -200°F (the typical temperature for LNG) and its body could crack, its stem could seize, or it could leak so badly it creates a hazardous buildup of liquefied gas. The first rule of selecting a cryogenic ball valve is: never use a standard valve rated for “low temperature”—only specify valves engineered explicitly for cryogenic service. That distinction is non-negotiable.
The second critical step is understanding your valve’s end connections. This isn’t just about how you attach it to the pipe—it’s about making sure the connection can handle both thermal expansion and contraction without failing. Cryogenic valves go through extreme temperature swings every time the system is cooled down from ambient to operating temp; that swing can cause metal pipes and valves to shrink by as much as 1/8 inch per foot of length. I’ve seen customers use screwed end connections for a small cryogenic transfer line, only to have the threads strip when the pipe shrank, leading to a full system shutdown. For most cryogenic applications, welded or flanged connections are the safe choice. Welded connections are ideal for permanent lines, as they eliminate any potential leak path at the joint. For applications that need to be disassembled periodically, like test skids or small batch processes, full-face flanged connections (with raised face or ring joint design, depending on pressure) are the standard. Never use threaded ends for cryogenic service unless it’s a very small, low-pressure line, and even then, insist on a cryogenically rated sealant—regular Teflon tape will become brittle at cryogenic temps and fail.
Next comes the body material, and this is where a lot of people cut corners, especially to save on upfront cost. The body of the valve is the structural backbone, so it has to be able to withstand not just the cryogenic temperature, but also pressure cycles and any physical impact on the line. The biggest mistake we see here is using carbon steel for cryogenic service. Most carbon steels become brittle below -40°F (-40°C), that’s the nil-ductility transition temperature (NDTT) for most standard carbon steels—below that, a hard impact could cause the body to shatter like glass. For cryogenic ball valves, the three approved body materials are 304 series stainless steel (specifically 304L, the low-carbon variant to avoid intergranular corrosion), 316 series stainless steel (316L is even better for corrosive cryogens like liquid oxygen), and brass for very low-pressure, low-temperature applications like laboratory cryogenic storage containers. Wait—you might be wondering: why not aluminum? Aluminum is lightweight and works well in cold, but it’s not strong enough for high-pressure cryogenic lines like LNG pipelines, so it’s limited to low-pressure, cryogenic storage. The key takeaway here: always check the material’s impact toughness at your exact operating temperature, not just its minimum rated temperature. A valve rated for -150°F made from 304L will work, but a valve made from the same 304L might fail at -200°F because its manufacturer didn’t test for impact toughness at that lower temp. Always ask for material test reports (MTRs) that confirm toughness at your specific operating temp—any reputable valve supplier will provide these without hesitation.
Now let’s talk about the ball and seat, two components that are at the heart of how a ball valve functions, and where cryogenic service causes the most leaks. The ball needs to be smooth and hard enough to create a tight seal, and at cryogenic temps, it also needs to maintain its shape—no warping. Most cryogenic ball valve balls are made from the same 304L or 316L stainless steel as the body, and many are coated with a hard, cryogenically suitable material like Stellite to reduce wear and friction. That’s important because when you open and close the valve, the ball spins against the seat, and at extremely low temps, friction can be high enough to strip the stem if the coating isn’t there.
The seat, however, is the part that most often causes leaks. Seats for cryogenic service can’t use standard Buna-N rubber or even standard Teflon (PTFE)—both become brittle at cryogenic temps, leading to gaps between the ball and seat that let liquid or gas escape. Instead, cryogenic seats use specialized materials, with the most common being reinforced PTFE (often called RPTFE) or PEEK (polyether ether ketone) for higher pressure applications, and even metal seats for extreme cases like liquid oxygen, where organic materials could catch fire if contaminated. But it’s not just the material—seat design matters too. The best cryogenic ball valves have a vented or pressure-relieving seat design, because if trapped cryogenic fluid between the ball and seats warms up, it can vaporize and create enough pressure to blow the seat out, leading to a massive leak. I’ve had to repair three valves last year where the user installed a standard valve with no pressure relief, and when they cycled the valve, the trapped fluid expanded and destroyed the seat. Always ask about the seat’s pressure relief feature—it’s non-negotiable for cryogenic service.
Then there’s the stem and packing, another frequent failure point. The stem is the part that connects the valve handle or actuator to the ball, and it has to seal the area where the stem passes through the valve body to prevent leaks. At cryogenic temps, the stem shrinks at a different rate than the packing material, creating a tiny gap that can leak. Standard packing (like graphite or rubber) can’t handle that differential shrinkage. Cryogenic valve packing is specially designed with flexible graphite rings, often with a backup seal made from a cryogenically compatible elastomer, that can expand and contract with the stem without leaking. We also recommend stem extensions for valves that need to be operated from above the cryogenic line—for example, if your line is buried or inside a cold box, a standard stem that’s too short will not only be hard to reach, but could also allow cold to travel up the stem to the handle, making it impossible to operate, and in some cases, causing the packing to leak because it’s too cold. Stem extensions are a low-cost add-on that prevents a huge number of operational issues.
Finally, don’t forget about testing and certification. A valve that says “cryogenic” on the tag isn’t necessarily tested for real-world service. The most important test for cryogenic ball valves is a cold seal test, where the valve is cooled down to the operating temperature and pressurized with a gas or liquid to check for leaks. We test every cryogenic valve we ship at -196°C (-321°F, the temperature of liquid nitrogen) at 150% of the valve’s working pressure, to make sure the seats don’t leak and the body doesn’t crack. Other certifications to look for include API 607 for fire safety (critical if you’re handling flammable cryogens like LNG or liquid propane) and ISO 15848 for fugitive emission control, which ensures the valve won’t release small amounts of gas to the atmosphere—a must for environmental compliance. Avoid any valve supplier that can’t provide proof of these tests and certifications; they’re cutting corners, and you’ll pay for it in downtime.

I know this sounds like a lot, but here’s the thing: selecting a cryogenic ball valve doesn’t have to be complicated if you focus on these five core factors: cryogenically rated design (not just low temp use), correct end connections, impact-tough body material, specialized seats and packing, and third-party tested certifications. I’ve spent my career working with customers to navigate these choices, because I’ve seen what happens when you pick the wrong valve—millions in lost production, safety hazards, and wasted money replacing valves every six months instead of every five years. If you’re working on a new cryogenic system, or having recurring issues with your current valves, don’t guess your way through the selection process. Reach out to our team to discuss your application, and we’ll help you pick the right cryogenic ball valve for your specific needs, no hidden fees, no pressure, just straight talk from someone who’s been doing this for nearly two decades. We’ll share test data, material specs, and even tips for installation to make sure your system runs smoothly from day one.
Check Valve 参考文献
- ASME B16.34: Valves – Flanged, Threaded, and Welding End
- API 6D: Pipeline Valves
- ASTM A352/A352M: Standard Specification for Steel Castings, Ferritic and Martensitic, for Pressure-Containing Parts, Suitable for Low-Temperature Service
- Control Valve Handbook, 5th Edition, Emerson Process Management
Zhejiang Poro Valve Manufacturing Co., Ltd.
With abundant experience, we are one of the most professional ball valve manufacturers and suppliers in China. We warmly welcome you to buy customized ball valve made in China here from our factory. If you have any enquiry about cooperation, please feel free to email us.
Address: PORO Ind. Park, Oubei Dongou Ind. Zone, Wenzhou, Zhejiang, China
E-mail: poro@cnporo.com
WebSite: https://www.cn-poro.com/
